Start with a safe, repeatable check
Confirm the material and thickness, inspect the nozzle and protective optics, check nozzle centering and gas quality, and compare the current recipe with the machine maker’s approved parameter chart. Make a small test cut and change one parameter at a time.
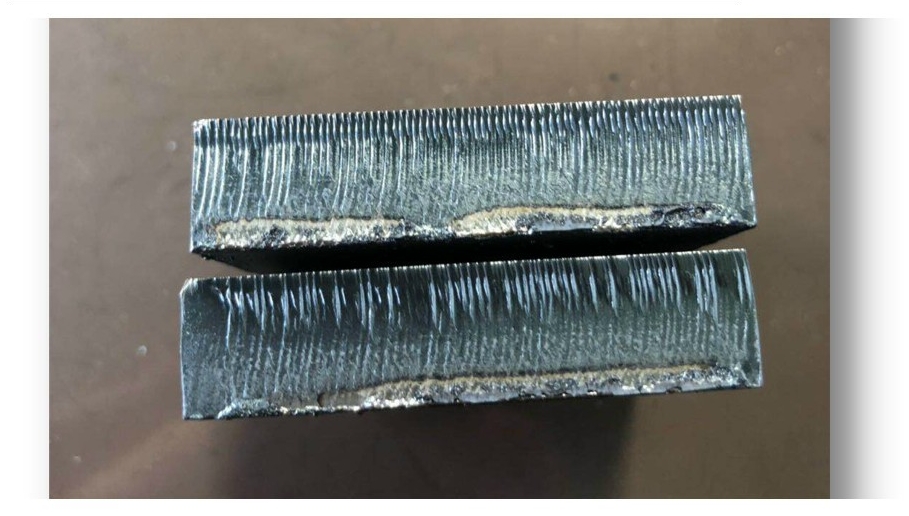
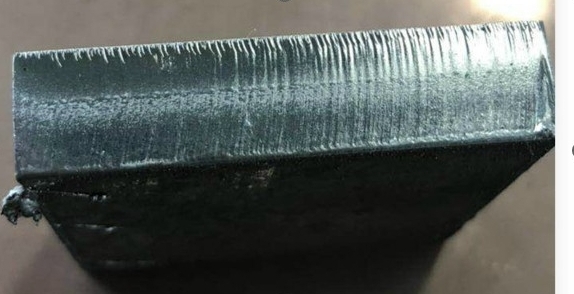
Coarse striations or overburn
Possible causes in the source include a nozzle that is too large, excessive cutting-gas pressure, or a speed that is too slow or too fast. Confirm the correct nozzle for the head and material, then adjust gas and speed only within the machine maker’s process window.
Cut does not pass through the sheet
A nozzle that is too small, an unsuitable focus position or insufficient gas may leave the cut incomplete. Check the nozzle and gas path, then adjust focus and pressure according to the approved recipe for that material and thickness.
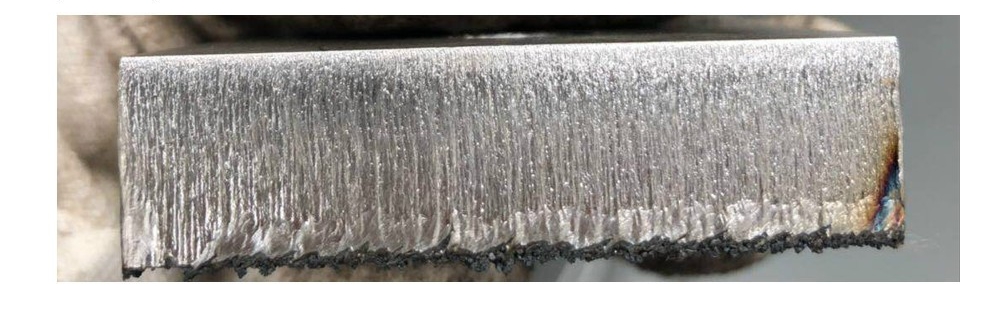
Rough stainless-steel cut or layer separation
The source associates this pattern with excessive negative focus, a small nozzle or excessive gas pressure. Check for unstable plasma or a blue glow, then verify focus, nozzle and gas against the exact machine recipe. Do not copy frequency or duty-cycle values from another machine.
Slag on the underside
A focus position that is too high, insufficient gas pressure or excessive cutting speed can contribute to underside slag. Inspect the optics and nozzle first; adjust focus, gas and speed in small steps, keeping all values within the equipment maker’s limits.
Top edge rougher than the underside
The source lists an oversized nozzle, insufficient positive focus or very low speed as possible causes. Confirm the material-specific nozzle and focus reference, then run a short test cut and tune speed using the approved chart.
Important parameter note
The source page includes nozzle-size and pressure examples, but those values are process-specific. They are not universal settings. Use the exact laser source, cutting head, material, thickness and gas recipe supplied by the equipment maker.
📸 Photo suggestion
Add a clear photo of the top and underside of the same test coupon, with the material, thickness, nozzle code and current process recipe recorded.
Contact PK LASER
Send photos or a short video of the cut together with the cutting-head model. Zalo: 0394 552 839; technical support: 0394 542 839.