Start with the exact material and machine recipe
Stainless-steel grade, thickness, surface condition, laser source and cutting head all affect the process. Begin with the machine or head manufacturer’s approved chart for the exact setup. Do not transfer nozzle diameters, pressure, focus offsets, frequency or duty-cycle values from another machine.
Select the nozzle from the approved chart
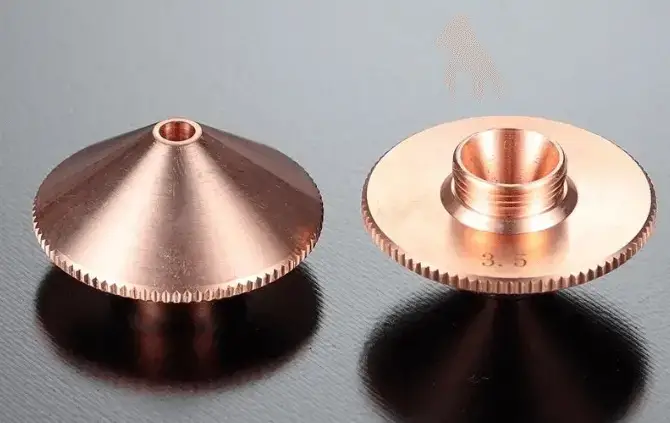
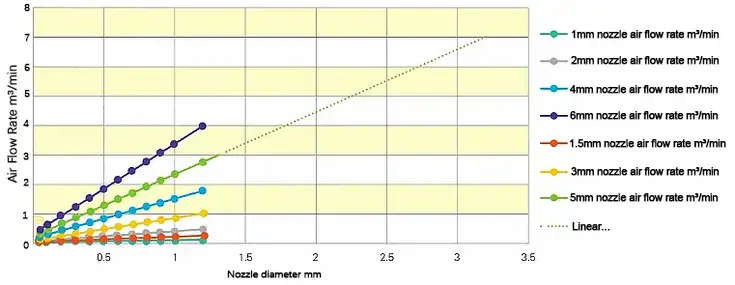
Nozzle geometry and bore influence assist-gas flow and melt removal. A nozzle that is too small, too large, damaged or off-center can reduce cut stability or damage the head. Match its type, size, mounting and condition to the head manual and process chart.
Choose assist gas for the required result
Oxygen, nitrogen and compressed air can produce different edge appearance and process behavior. The choice depends on the material, thickness, machine capability, required oxidation level and downstream finishing. Use the gas supplier’s purity specification and the machine maker’s flow and pressure data for the exact recipe.
Set focus and alignment using approved methods
Focus position and beam-to-nozzle centering affect cut quality and nozzle condition. Use the cutting head’s calibration and alignment procedure. Do not tape over the nozzle or output and fire an improvised beam test; alignment work should be done only with approved equipment and trained personnel.
Treat pulse and frequency settings as model-specific
Frequency, pulse duration, duty cycle and peak power interact. Small changes can alter cut-through, striation and edge color, but the response depends on the source and head. Use the validated recipe, make controlled test cuts where permitted and change one approved value at a time. Stop if the beam, head or material behaves abnormally.
Record and verify the test
Use a test coupon of the production grade and thickness. Record the nozzle, gas, focus reference and approved source settings, then inspect cut-through, top and bottom edges, dross and repeatability. Keep the settings that meet the drawing and process requirements, not simply the smoothest-looking sample.
Photo suggestion
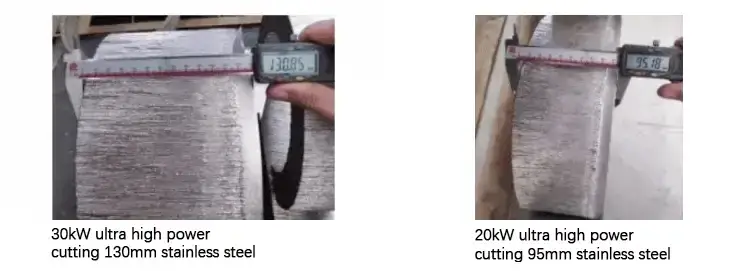
Show a labeled stainless-steel test coupon and the machine’s approved process chart or nozzle identification. Do not publish unverified pressure, purity, focus or pulse numbers as general recommendations.